


Heavy-Duty Industrial Pallet Racks – High Load Capacity, Durability, and Safety


Nowadays, businesses need solutions that optimize storage space more efficiently, increase durability, and provide greater flexibility. Therefore, heavy duty pallet racks have become a top choice, especially when manufactured by experienced heavy duty pallet rack manufacturers.
These racks are not merely storage equipment—they are a key part of operational optimization strategies, reducing costs and accelerating goods handling processes. The durability provided by the systems from experienced heavy duty pallet rack manufacturers translates directly into substantial long-term cost savings.
By utilizing specialized, high-grade steel and stringent quality control, these heavy duty pallet rack manufacturers ensure their products minimize structural deflection and resist damage from continuous heavy use, far exceeding the lifespan of standard racks. This increased durability drastically reduces the need for frequent repairs and replacements, turning the initial investment into a highly reliable and cost-effective foundation for stable, high-volume logistics operations.
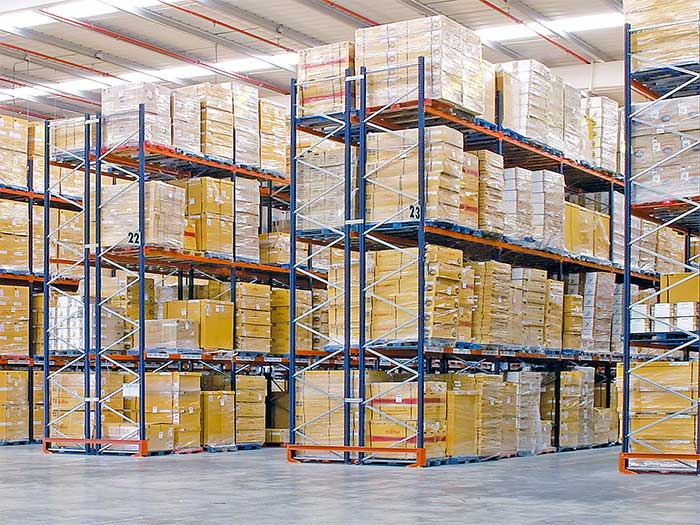
Why Heavy-Duty Pallet Racks Are Preferred in Industrial Warehouses
The core difference between heavy-duty pallet racks and conventional storage solutions lies in their ability to withstand extremely high loads and their structural durability.
Massive Load Capacity – Absolute Safety
A high-quality heavy rack system is designed to handle the heaviest pallets, from raw materials and packed finished products to machinery components. On average, each rack level can support 800 kg to 6,000 kg or more, depending on the design.
- Space Optimization: Stacking multiple tiers takes full advantage of warehouse height, increasing storage density while maintaining structural integrity.
- Risk Minimization: Made from high-quality steel, the beams and uprights are resistant to deformation and impact, greatly reducing the risk of collapse—a constant concern for warehouse managers. This is why the materials used in steel storage racks are strictly tested.
The stringent testing and use of high-yield steel are non-negotiable standards upheld by professional heavy duty pallet rack manufacturers. By adhering strictly to RMI or EN load-bearing specifications, the heavy duty pallet rack manufacturers guarantee that the systems not only support the extreme weights mentioned but also maintain structural stability under continuous operational stresses.
This commitment to engineered safety and material integrity transforms the heavy rack system from a simple storage unit into a certified, critical asset that is essential for both maximizing density and safeguarding personnel and inventory.
Maximizing Height and Floor Space with Industrial Racking
As warehouse real estate costs continue to rise, vertical space optimization, also known as industrial racking, has become a priority. Instead of expanding the floor area, businesses invest in high-rise rack systems to make the most of the “air space.”
- Economic Benefits: Initial investment costs are quickly offset by savings on leasing or constructing additional floor space.
- Easy Integration: Compatible with modern lifting equipment (Reach Trucks, VNA – Very Narrow Aisle forklifts) for operations at high elevations.
This shift toward vertical storage necessitates robust engineering, making the choice of heavy duty pallet rack manufacturers paramount. Only certified heavy duty pallet rack manufacturers can provide the high-tolerance, structurally sound uprights and beams required to safely support massive loads at extreme heights.
Their specialization ensures that the high-rise systems are not only perfectly integrated with VNA or Reach Trucks but also comply with stringent seismic and load-bearing standards, guaranteeing the long-term safety and maximum return on investment from optimized vertical space.
Most Common Types of Heavy-Duty Pallet Racks Today
Each business model and type of goods requires a tailored storage solution. Understanding different heavy rack systems helps make smarter investment decisions.
Standard Australian Heavy-Duty Racks – Core Product Line
- Load capacity: 500 – 5,000 kg/level
- Types: Selective, Double Deep, Drive-In, Push-Back, Pallet Flow, Shuttle, Mobile
- Steel structure warranty: 15 yearsv
This wide array of systems, ranging from Selective to Mobile, is standardized and backed by the expertise of heavy duty pallet rack manufacturers. By offering versatile solutions with load capacities from 500 – 5,000 kg/level and a structural warranty up to 15 years, the heavy duty pallet rack manufacturers ensure businesses receive a high-quality, flexible, and reliable storage foundation suitable for any industrial operation.
Cantilever Racks – Solution for Long, Bulky Items
- Steel coils, pipes, lumber, aluminum sheets, moulds…
- Single/double arms, load capacity: 500 – 5,000 kg/arm
- Flexible or fixed installation, outdoor use (hot-dip galvanized)
This specialized horizontal storage capacity is expertly engineered by heavy duty pallet rack manufacturers. By designing Cantilever Racks with robust single/double arms and load capacities up to 5,000 kg/arm, the heavy duty pallet rack manufacturers provide a vital, custom-engineered solution for optimally storing long, awkward materials (pipes, lumber) safely, even offering hot-dip galvanized options for reliable outdoor durability.
- Load capacity: 300 – 800 kg/level
- Tool-free assembly in 5 minutes
- 5-layer powder coating: blue – orange – gray
- Suitable for spare parts warehouses, automotive parts, and e-commerce warehouses
This system’s rapid, tool-free assembly and durable 5-layer coating, critical for high-turnover sectors like e-commerce and automotive, are guaranteed features provided by the heavy duty pallet rack manufacturers. By delivering a stable structure with high-grade steel and flexible load capacities (300–800 kg/level), the heavy duty pallet rack manufacturers ensures businesses gain a highly adaptable, cost-efficient, and long-lasting storage solution optimized for varied medium-weight inventory.
Teardrop Pallet Rack – RMI Standard
- Compatible with teardrop accessories from Interlake, Ridg-U-Rak, Steel King…
- Teardrop hole spacing: 50.8mm (2 inch)
- Easy replacement and expansion for businesses with existing U.S.-standard racks
This standardized compatibility ensures seamless integration and quick access to parts across the industry, a crucial feature guaranteed by the heavy duty pallet rack manufacturers. By adhering to the precise 50.8mm (2-inch) teardrop hole spacing and RMI standards, the heavy duty pallet rack manufacturers provide businesses with a future-proof, highly flexible, and universally supported solution for easy replacement and scalable expansion.
- Column Guard (protective post)
- Wire Mesh Deck & Back Mesh
- Pallet stop bars, carton support beams
The strategic use of these essential accessories—from Column Guards to Pallet Stop Bars—is fully supported by reliable heavy duty pallet rack manufacturers. By integrating these components, the heavy duty pallet rack manufacturers ensure that the system not only meets extreme load requirements but also provides comprehensive protection, minimizing forklift damage and maximizing safety compliance across all levels of the heavy-duty racking installation.
- Load capacity: 500 – 2,000 kg/m²
- Easy installation, no special tools required
- Ensures natural light and ventilation
This versatility and safety enhancement, inherent to the steel Mesh Deck, is ensured by the quality control of the heavy duty pallet rack manufacturers. By integrating these fire-safe, high load-capacity decks into their systems, the heavy duty pallet rack manufacturers deliver solutions that not only optimize light and airflow but also significantly boost overall warehouse safety and compliance without sacrificing ease of assembly.
Golden Criteria for Choosing a Reputable Heavy Duty Pallet Rack Manufacturer
This is the most critical section where your business looks for a partner that can ensure long-term investment quality. A professional heavy-duty pallet rack manufacturer doesn’t just sell products—they deliver safety and performance solutions.
Quality Certification and International Standards
A reputable manufacturer must prove product quality through strict international standards, not just verbal promises.
- FEM/RMI Standards: Standards from the European Materials Handling Federation (FEM) or the Rack Manufacturers Institute (RMI) in the U.S. clearly demonstrate structural durability, load-bearing capacity, and safety.
- Steel Type and Thickness: Detailed specifications of the steel used (e.g., JIS standard cold-rolled steel or equivalent) and the actual thickness of beams and uprights are essential. Only high-quality raw materials ensure a 10 – 15 year lifespan for steel storage racks.
Professional heavy duty pallet rack manufacturers go beyond providing standard products—they offer tailored design solutions to meet the unique requirements of each warehouse. By assessing pallet types, product dimensions, load distribution, and forklift operations, these manufacturers optimize rack layouts for maximum storage efficiency and material flow.
Their engineering expertise ensures that every system not only supports heavy loads safely but also integrates seamlessly with modern warehouse equipment, such as VNA and Reach Trucks, delivering a reliable, high-performance storage solution for long-term operations.
Custom Design Capability
Every warehouse is unique. A competent heavy-duty pallet rack manufacturer should have an experienced engineering team to:
- Assess Loads: Accurately calculate static and dynamic loads based on pallet type, product dimensions, and forklifts used.
- Optimize Layout Design: Propose industrial racking solutions suited to material flow, throughput frequency, and spatial constraints of the warehouse.
This in-depth engineering capability, provided by the heavy duty pallet rack manufacturer, is crucial for translating operational data into a structurally sound design. By meticulously analyzing factors like beam deflection and seismic stress, the manufacturer ensures the final high-capacity system not only fits the physical space but also strictly complies with international safety standards (RMI/EN).
This commitment from the heavy duty pallet rack manufacturer eliminates costly design errors and guarantees that the heavy-duty racking provides a safe, highly efficient, and long-term foundation for the client’s unique logistics workflow.
Professional Installation, Maintenance & Warranty Services
The installation process directly affects the safety of the heavy rack system.
- Professional Installation: The installation team must follow technical drawings and strict safety procedures.
- Clear Warranty Policy: Long-term structural warranty and support for periodic inspections ensure ongoing safety and performance of the pallet racks.
This commitment to ongoing safety post-installation differentiates a premier heavy duty pallet rack manufacturer. They view the warranty not as a legal obligation, but as an extension of their quality guarantee, providing essential follow-up support like specialized inspection training and maintenance guidance.
By ensuring every connection is precise and every safety measure is implemented correctly by their certified team, the heavy duty pallet rack manufacturer minimizes structural liabilities, maximizes the lifespan of the system, and secures the client’s investment against premature failure.
Conclusion
Investing in high-quality heavy duty pallet racks is no longer merely a procurement decision; it is a strategic operational mandate for modern industrial warehouses facing escalating real estate costs and increasing demands for safety and throughput. The core value of these systems—massively enhanced structural durability, maximized vertical storage, and reduced risk of catastrophic failure—directly translates into predictable, long-term economic advantages.
By partnering with a heavy duty pallet rack manufacturer that strictly adheres to international standards (like RMI and FEM) and provides expertise in custom design and professional installation, businesses secure more than just steel frames. They acquire a certified, future-proof foundation for their entire supply chain, enabling seamless integration with automation (VNA, Reach Trucks) and ensuring compliance with stringent safety regulations.
Ultimately, a strategically implemented heavy-duty racking system is the most reliable tool for optimizing every square meter, guaranteeing worker safety, and ensuring sustainable, long-term profitability in high-volume, dynamic logistics
Contact BHD Vietnam Today
If you are seeking a solution to optimize warehouse storage space according to international standards, get professional consultation, design advice, quotations, and on-site survey from our experienced experts.


