


Industrial Pallet Rack Manufacturers: The Optimal Racking System for Factories and Warehouses


Introduction
As manufacturing and logistics continue to expand, factories and warehouses are facing increasing pressure on storage capacity. Choosing a reputable industrial pallet rack manufacturers are critical factor that helps businesses optimize space, increase productivity, and ensure warehouse safety.
For BHD – Palletrack.vn, industrial racking systems not only provide efficient storage but also support inventory management, reduce handling time, and minimize the risk of product damage. Industrial shelving systems and steel racking solutions enable businesses to organize warehouse layouts scientifically, reduce operational costs, and maximize the functionality of every square meter.
The complexity of scaling up storage capacity safely underscores the necessity of partnering with certified industrial pallet rack manufacturers. Top-tier industrial pallet rack manufacturers provide more than just steel; they deliver expertly engineered, compliant solutions (meeting RMI, ANSI, or EN standards) designed to handle extreme load capacities and seismic stresses.
This engineering precision is vital for maximizing vertical space while minimizing the footprint, ensuring that the heavy-duty racking systems supplied by the industrial pallet rack manufacturers serve as a durable, long-term asset that guarantees both operational efficiency and workplace safety.
1. Overview of Industrial Pallet Racking
Industrial pallet racking is a specialized storage solution designed for factories, industrial warehouses, and logistics centers. Industrial pallet racking manufacturers develop these systems based on each business’s operational needs, including:
- Optimized storage capacity: Maximizing warehouse height and depth to store multi-tier pallets efficiently.
- Easy access to goods: Operators and forklifts can handle each pallet directly without needing to move other pallets.
- Efficient inventory management: Every pallet has a fixed, clearly defined position, reducing errors and ensuring easier stock checking.
When integrated with other industrial storage components, such as a dedicated factory rack system and robust steel storage system, businesses can seamlessly implement smart-warehouse trends. Beyond space optimization and inventory control, industrial pallet racking also delivers significant advantages in safety and operational flexibility.
Thanks to its robust structure made from high-strength steel and precisely engineered load-bearing beams, the weight of pallets and stored goods is evenly distributed across the upright frames and base plates—minimizing deformation and reducing the risk of rack collapse.
This level of engineering integrity is consistently guaranteed when choosing solutions from professional industrial pallet rack manufacturers, who adhere to strict safety and quality standards during the entire production process.”
2. Structure and Operating Principles
Main Frame (Upright Frame)
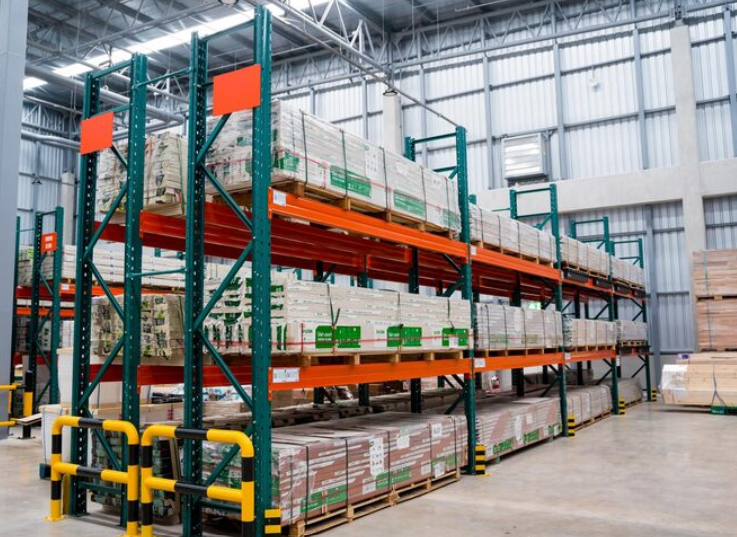
The main frame of industrial pallet racking is made from high-strength structural steel, designed to withstand the full load of pallets and stored goods. This structure ensures even load distribution to the base plates, minimizing bending, sagging, or long-term deformation. The frame is also reinforced to maintain stability even under continuous warehouse operations.
Horizontal Beams
Horizontal beams bear the direct load of the pallets and work together with the upright frame to ensure maximum stability for the entire racking system. Even load distribution not only reduces the risk of pallet damage but also protects stored goods and increases the overall lifespan of the racking system.
Decking (Shelf Surface)
The decking can be steel panels, wire mesh decks, or industrial wooden boards, providing a stable surface that prevents pallets from shifting during forklift operations. Wire mesh decks, in particular, enhance warehouse safety by allowing light penetration and ensuring proper airflow for fire suppression systems. Choosing the appropriate decking material, a critical recommendation made by expert industrial pallet rack manufacturers, often varies based on load type and environmental conditions (such as cold storage), and is crucial for protecting the goods and optimizing long-term storage efficiency.
Safety Accessories
Safety accessories such as guards, mesh panels, safety bars, and signage are installed to reduce collisions, prevent falling objects, and enhance operator safety. These components are especially important in cold storage, heavy-industry warehouses, or FMCG facilities with dense forklift movement.
Operating Principles
The system operates based on even load distribution from pallets through the horizontal beams down to the upright frames and base plates. This optimal load handling is a hallmark of design from leading industrial pallet rack manufacturers. Adjustable beam levels allow the storage of various pallet sizes and product types, helping businesses optimize warehouse space and increase inventory management efficiency.
3. Key Advantages
Easy Access
The racking system allows operators and forklifts to access each pallet individually without moving other pallets. This design supports modern warehousing trends, reduces handling time, and minimizes the risk of product damage during loading and unloading.
Space Optimization
The ability to adjust rack levels flexibly in height and spacing to accommodate diverse pallet sizes and product categories is essential. Industrial pallet rack manufacturers ensure this flexibility, allowing for proper vertical arrangement which maximizes storage density while maintaining both safety standards and ease of inventory management
Operational Flexibility
System components can be assembled, dismantled, or relocated without affecting other racks. This makes the system especially suitable for factory racking setups, enabling intuitive warehouse management, saving time, and improving overall operational efficiency.
4. Benefits of Partnering with industrial pallet rack manufacturers
Choosing professional industrial pallet rack manufacturers offers businesses several advantages:
- Ensured warehouse safety: Racks are designed and manufactured according to international standards.
- Guided maintenance: Regular rack maintenance instructions help extend the system’s lifespan.
- Support for modern storage trends: Enables visual inventory management and efficient stock control.
- Reduced design errors: Expertise from experienced manufacturers minimizes mistakes in warehouse rack planning.
Partnering with a professional industrial pallet rack manufacturer not only ensures confidence in the quality and durability of the racking system but also delivers long-term operational efficiency.
With their experience and expertise, manufacturers can advise on scientifically organized warehouse layouts, optimize storage space, and seamlessly integrate steel storage racks, warehouse shelving and factory racking systems.
This allows businesses to easily monitor inventory, improve loading and unloading productivity, and successfully implement smart warehouse management strategies.
Ultimately, the competitive advantage gained through increased safety, optimized space, and enhanced operational speed proves the value of choosing among leading industrial pallet rack manufacturers rather than opting for uncertified, lower-cost alternatives.
5. Applications in Different Warehouse Types
Heavy Industrial Warehouses
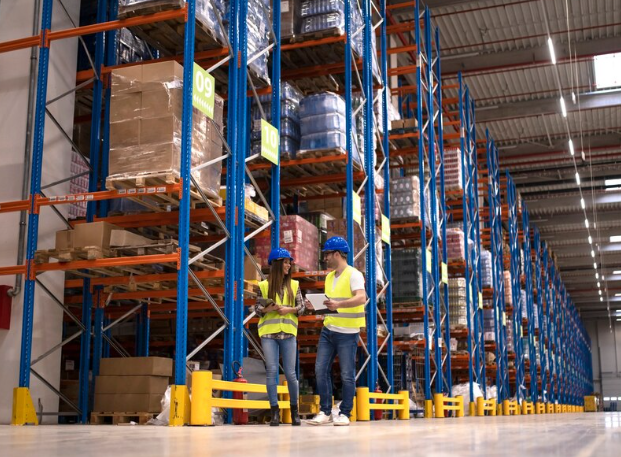
For warehouses storing heavy pallets, bulky components, or large materials, the robust steel frame of industrial pallet racks reduces the risk of collapse, protects goods, and ensures operator safety. This core structural strength is a hallmark provided by expert industrial pallet rack manufacturers.
By adhering to strict engineering standards, a certified industrial pallet rack manufacturer guarantees that the robust steel framework can reliably handle extreme loads, significantly minimizing the risk of failure and cementing the system as a safe, long-term asset essential for heavy-duty warehouse environments.
FMCG Warehouses
Fast-moving consumer goods require frequent loading and unloading. Racking systems optimize handling, increase productivity, and simplify inventory management. Industrial pallet rack manufacturers specialize in designing systems for these high-throughput environments, ensuring the racks provide both structural stability for rapid operations and the necessary accessibility to maintain high efficiency.
Cold Storage Warehouses
Warehouses storing food, milk, or meat require racks capable of withstanding cold and humid conditions. Industrial steel storage racks are specially designed to protect goods while ensuring safe operations under low-temperature environments.
6. Challenges in Implementing Industrial Pallet Racks
Diverse Inventory
Each type of goods has specific storage requirements. Heavy or bulky items require high-load-bearing racks, while fast-moving consumer goods or cold storage items need racks that are easily accessible and moisture-resistant. Selecting the right rack protects goods, reduces the risk of damage, and ensures warehouse safety.
Space Optimization
The spacing between rack levels, height, and depth must be scientifically arranged to maximize warehouse space while allowing easy access for staff and forklifts. Proper layout also supports efficient operations and smooth warehouse workflow.
Maintenance and Inspection
Components such as uprights, beams, bolts, and welds need regular inspection. Routine maintenance extends the system’s lifespan and minimizes operational issues. This focus on component integrity requires certified materials, a guarantee provided exclusively by reliable industrial pallet rack manufacturers.
By adhering to meticulous manufacturing standards for every beam and upright, the industrial pallet rack manufacturers ensure that routine maintenance is effective, maximizing the system’s longevity and safeguarding the entire heavy-duty operation.
Initial Investment Cost
High-quality racking systems may require significant upfront investment. However, due to their durability, optimized storage capacity, and reduced risk of goods damage, businesses can save long-term operating costs.
7. Conclusion
Despite the challenges of diverse inventory and initial investment, partnering with experienced industrial pallet rack manufacturers remains the most critical strategic decision. They provide tailored solutions to optimize space, ensure structural integrity, and offer long-term support, transforming the upfront cost into sustainable operational efficiency and comprehensive warehouse safety.
This partnership with reputable industrial pallet rack manufacturers extends far beyond the initial sale; it establishes a commitment to the longevity of the storage asset. By utilizing specialized materials and advanced engineering, top industrial pallet rack manufacturers guarantee systems that withstand the constant demands of heavy industrial use and complex logistics operations.
This dedication to quality ensures the upfront investment yields maximum return, transforming the warehouse infrastructure into a highly reliable, compliant, and adaptable tool that sustains optimal throughput for decades.
Ready to Optimize Your Warehouse?
Contact BHD – Palletrack.vn today for a free quote and design layout for your Heavy-Duty Pallet Racking System. Ensure absolute safety and increase storage capacity by 40%!


