


Industrial Drive-in Pallet Racks – Optimize Space for Large Warehouses and Cold Storage


Introduction
The demand for storage in industrial warehouses, cold storage facilities, and logistics centers is rapidly increasing, especially when warehouse space is limited but inventory volumes are high. In this context, drive-in pallet racks have become an optimal solution to maximize storage density while maintaining efficient operations.
Unlike conventional pallet racks, drive-in racks make full use of warehouse depth, reducing aisles and allowing multiple pallets of the same type to be stored in a single lane. This system is particularly suitable for businesses that manage long-shelf-life products or require high-volume inbound and outbound handling.
BHD – Palletrack.vn provides expert insights into applying drive-in pallet racks, helping businesses optimize space, increase storage efficiency, and reduce operating costs while ensuring safety and flexibility for future needs.
1. Structure and Operating Principle of Drive-In Racks
A standard drive-in pallet rack system consists of the following main components:
- Upright Frames: Made of high-strength steel, these frames bear the full load of stacked pallets. They ensure structural stability and reduce the risk of deformation under heavy loads.
- Horizontal Beams: Connect the upright frames, distribute loads evenly, and support the pallets.
- Pallet Guides/Rails: Direct the movement of pallets into the rack lanes, allowing forklifts to enter directly for loading or picking.
- Support Beams and Wire Decking: Assist in distributing weight evenly, enhance stability, and prevent pallets from sagging or falling.
- Safety Rails, Stairs, and Signage: Ensure safe operation, guiding the movement of staff and forklifts within the warehouse.
Operating Principle:
Drive-in pallet racks operate on a system of rails connected between upright frames. When a front pallet is removed, the rear pallet moves forward via gravity or guided mechanisms, enabling continuous warehouse operation, reducing handling time, and increasing inbound/outbound efficiency.
This mechanism embodies the concept of a smart warehouse, where businesses prioritize space optimization and operational efficiency.
2. Advantages of Drive-In Racks
Maximizes Storage Space
Drive-in pallet racks utilize the full depth of the warehouse, reducing unnecessary aisles. This allows businesses to increase storage capacity 2–3 times without expanding the warehouse or adding floors.
Ideal for Homogeneous Inventory
With the Last-In-First-Out (LIFO) principle, this system is perfect for items of the same type or with similar shelf life, such as cold storage food, FMCG products, or heavy industrial goods.
Fast and Efficient Operation
Forklifts can enter the rack lanes directly, minimizing handling steps and reducing loading/unloading time. The system suits modern warehouse trends, prioritizing operational speed and space optimization.
Cost Savings
Compared to building new warehouse space or expanding existing facilities, investing in drive-in racks saves on construction costs, permits, and labor.
3. Applications of Drive-in Racks
Cold Storage
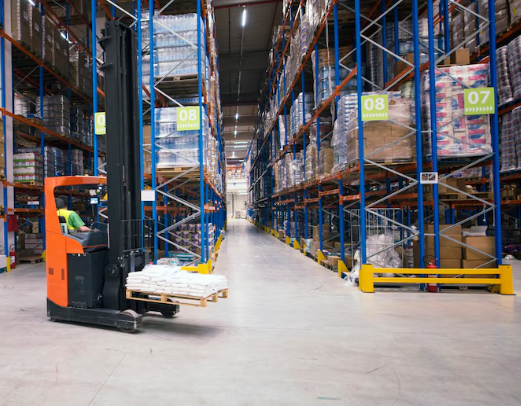
In warehouses that require strict temperature control, such as frozen food, milk, meat, and seafood storage, maximizing the depth of the warehouse is crucial. Drive-in pallet racks help reduce empty aisles and keep stacked pallets stable. Thanks to the continuous operation mechanism, warehouse staff do not need to move excessively, reducing handling time while ensuring efficient and safe goods in-and-out processes.
FMCG Warehouses
Fast-moving consumer goods (FMCG) need frequent in-and-out operations to avoid long-term storage. Drive-in racks reduce the number of forklift movements, increase operational productivity, and the deep storage area maximizes space utilization, lowers labor costs, and allows easy implementation of the FIFO (First-In-First-Out) system to ensure goods are circulated on time.
Heavy Industrial Warehouses
Pallets containing heavy goods or large components require high-load bearing systems. The sturdy steel frames combined with durable guide rails ensure safe pallet movement without sagging or damage. Drive-in racks allow multiple pallets to be stacked in a single aisle, optimizing space while maintaining operational safety and aligning with smart warehouse trends.
4. Accessories and Benefits
To optimize operation and warehouse safety, accompanying accessories are essential:
- Connector Beams: Maintain spacing and link the upright frames, enhancing overall rigidity and stability of the system.
- Support Beams: Support pallets, distribute loads evenly, and reduce the risk of pallet sagging or breaking.
- Upright Protectors: Protect against forklift impacts, extending the lifespan of the rack frame.
- Barriers: Prevent direct collisions from forklifts or other equipment, protecting aisles and rack columns.
- Wire Decks: Distribute loads and prevent pallets from falling, enhancing operational safety.
With these accessories, the drive-in pallet rack system operates flexibly, is easy to maintain, and can be expanded when needed. They help avoid common warehouse rack design mistakes such as instability, safety hazards, or underutilization of space.
5. Operation and Maintenance Guidelines
To ensure smooth operation and extend the lifespan of the system, regular warehouse rack maintenance is crucial:
Load Check
Before the operation, businesses need to clearly determine the maximum load per pallet and for the entire rack system. Adhering to the design load prevents beam sagging, pallet breakage, or frame damage, while ensuring the safety of personnel and goods. Each pallet’s weight should be considered before placing it on the rack, especially in heavy-duty industrial warehouses.
Guardrails and Signage
Proper-height guardrails and clear signage are essential for warehouse safety. Guardrails not only protect staff moving on the rack levels but also prevent pallets from sliding off. Signage indicating aisles, load limits, and restricted areas helps staff operate safely and minimizes forklift collision risks.
Bolts and Welds Inspection
Anchor bolts and welds are the primary load-bearing points of the drive-in pallet rack system. Regular inspections, tightening bolts, and checking welds help detect early signs of loosening, cracks, or wear, reducing the risk of damage and prolonging the system’s lifespan.
Anti-Rust Coating
The steel surfaces of the racks should be checked regularly for signs of rust. If detected, immediate anti-rust painting should be applied to protect the frame, maintain durability and aesthetics, and prevent structural weakening due to metal corrosion.
Periodic Inspection
To ensure continuous and safe operation, businesses should conduct periodic inspections according to the manufacturer’s guidelines, at least once every 12 months. Inspection procedures include checking load capacity, bolts, welds, paint condition, and overall rack safety, enabling effective maintenance and preventing unnecessary incidents.
6. Warehouse Design and Layout Considerations
When implementing a drive-in pallet rack system, attention should be paid to the following points to avoid errors:
- Rack Height and Depth: Determine accurately to ensure forklifts can move easily and maximize space utilization.
- Material Flow: Design clear aisles and distinct inbound/outbound areas.
- Maximum Load: Do not exceed the design limit to ensure rack safety.
- Protective Accessories Layout: Components such as connector bars, barriers, and steel mesh should be properly positioned. This not only reduces collision risks but also creates an efficient storage system, demonstrating a practical and well-planned warehouse layout.
7. Optimizing Efficiency and Modern Storage Trends
The drive-in pallet rack system offers numerous long-term benefits:
- Improved Operational Efficiency: Reduces handling time and optimizes material flow.
- Space Optimization: Effectively utilizes warehouse depth and height, combined with high-density storage solutions.
- Enhanced Safety: Minimizes risks of collisions and rack collapses.
- Easy Expansion: Adapts to layout changes without the need for additional construction.
This system aligns perfectly with the smart warehouse trend, where businesses aim for automated operations, space optimization, and cost reduction. Additionally, drive-in pallet racks facilitate inventory management according to FIFO (First-In-First-Out) or LIFO (Last-In-First-Out) principles, depending on the type of goods.
From a cost perspective, the high density achieved by the drive-in pallet rack system translates directly into lower square footage costs for storing the same volume of goods compared to traditional selective racking. This makes it an economically sound choice for storing large quantities of homogeneous products that do not require high selectivity.
Furthermore, the robust structural design of the drive-in pallet rack is engineered for endurance, providing a sustainable, long-term storage foundation that minimizes future maintenance and replacement expenses, ensuring a strong return on investment for high-volume storage needs.
Consequently, during warehouse design, companies can strategically plan the layout of drive-in racks to maximize space utilization while ensuring smooth and efficient material flow. This strategic design focus ensures that the drive-in pallet rack system not only delivers maximum storage density but also integrates flawlessly with the overall logistics flow.
By precisely mapping out the drive-in pallet rack layout during the initial design phase, businesses guarantee optimized travel paths, minimize congestion, and directly contribute to the swift, efficient movement of high-volume goods through the facility.
8. Conclusion
Drive-in pallet racks are an optimal solution for businesses that need to:
- Store large quantities of uniform goods.
- Maximize warehouse space without expanding or building new facilities.
- Optimize operations while reducing costs and risks.
When properly implemented and combined with protective accessories, drive-in racks ensure stable and safe warehouse operations. This makes them a long-term, flexible, and efficient choice, suitable for cold storage, FMCG warehouses, and heavy industrial storage facilities.
In essence, choosing the drive-in pallet rack system is a strategic decision that reflects modern logistics priorities. Its inherent structural integrity, combined with the ability to handle various storage environments like cold storage, confirms its versatility and reliability.
Businesses that utilize the drive-in pallet rack not only achieve superior space utilization but also embed a foundational element of stability into their supply chain. This investment ensures stable inventory management, minimizes the long-term risk of structural failure, and provides a durable, cost-effective solution for dense, high-volume storage requirements across diverse industries.
Triple Your Warehouse Storage Capacity!
Maximize your warehouse depth with specialized Drive-In Pallet Racks from BHD – Palletrack.vn. Get consultation on high-density storage solutions, perfect for cold storage and homogeneous inventory (LIFO/FIFO).


